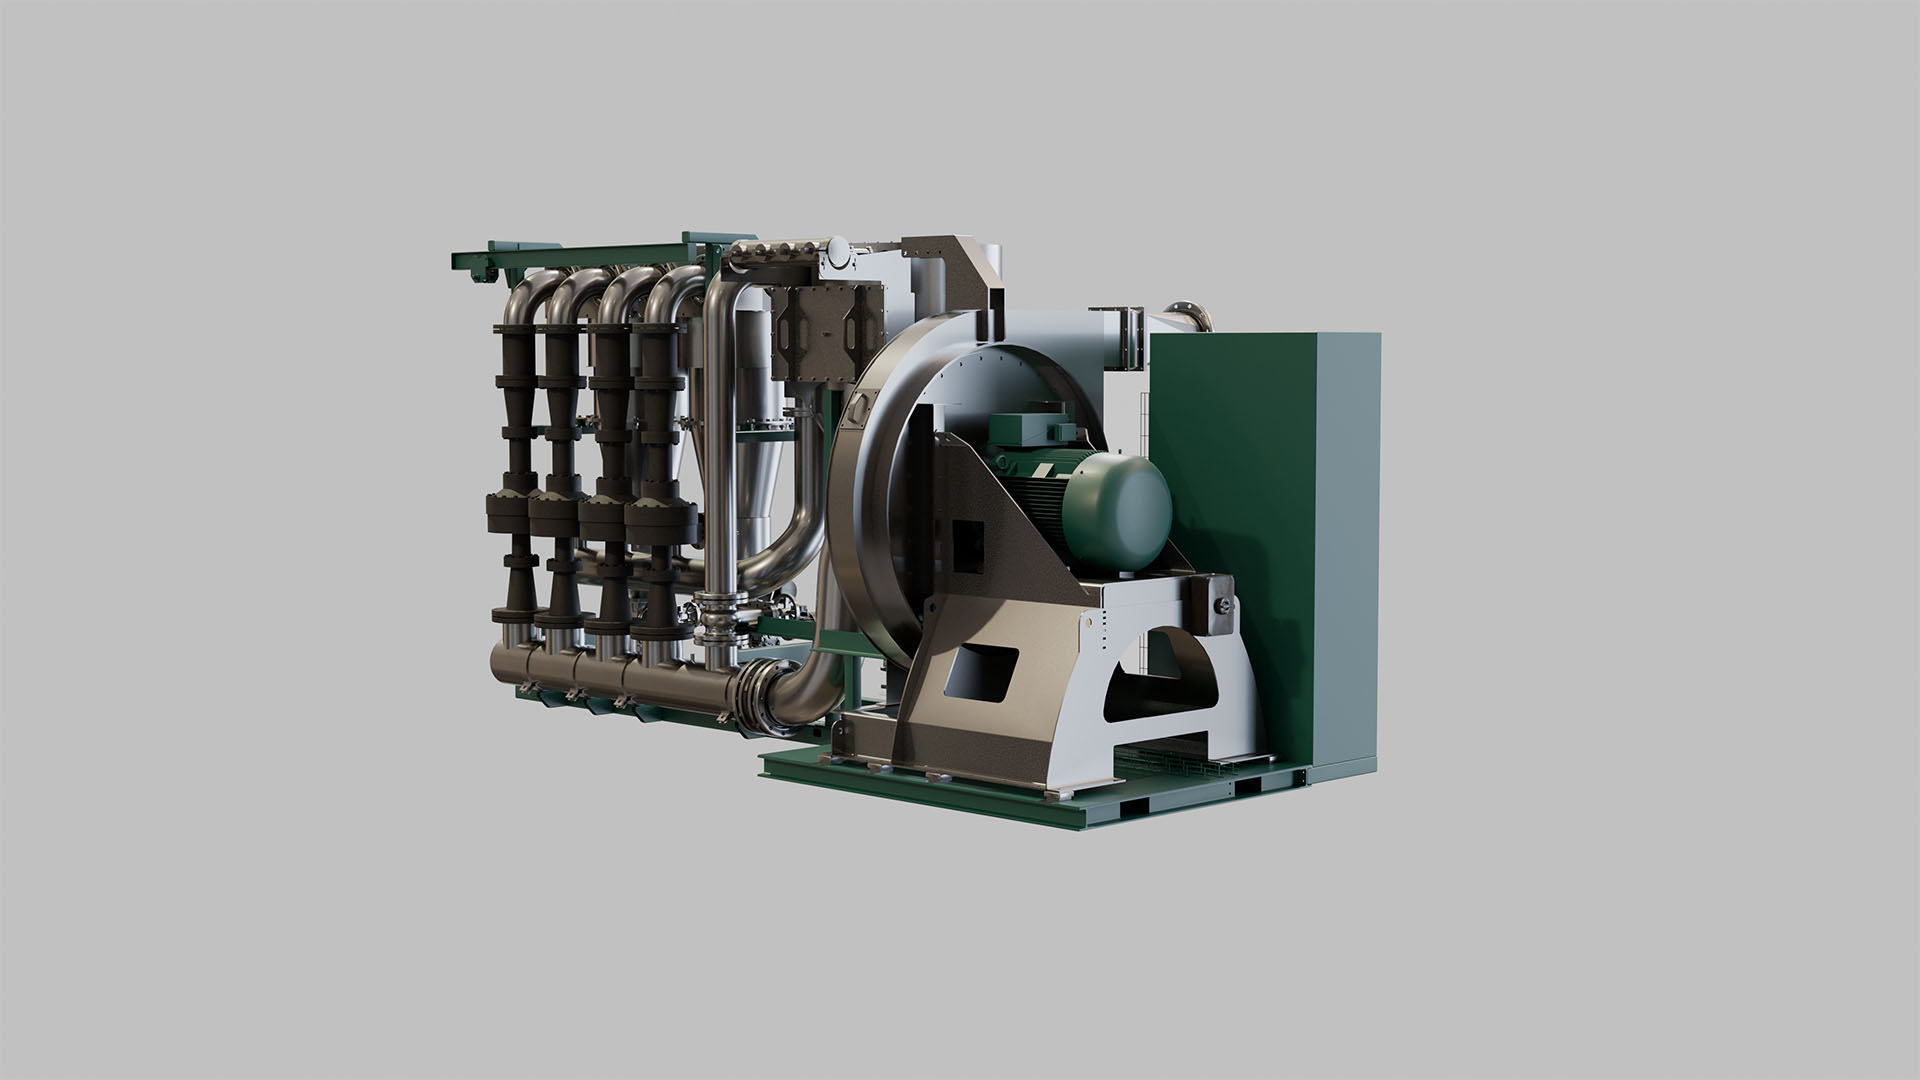

DC202 & DC402
flow-dynamic dust separators
A whole new category of industrial dust control equipment for demanding environments
Flow-dynamic dust separation
Filtrabit’s patented innovation for separating fine dust particles from gases is based on the principles of flow-dynamics and has created an entirely new category of dust control equipment for heavy industry.
Unprecedented performance of the separation core at the heart of the technology enables industrial clients to reduce their particulate emissions and meet strict environmental regulations, entirely without the use of water.
The side streams of immediately reusable raw materials captured by the technology create circular economy benefits on multiple levels, including reduced net CO2 emissions.
Modular units on the spot
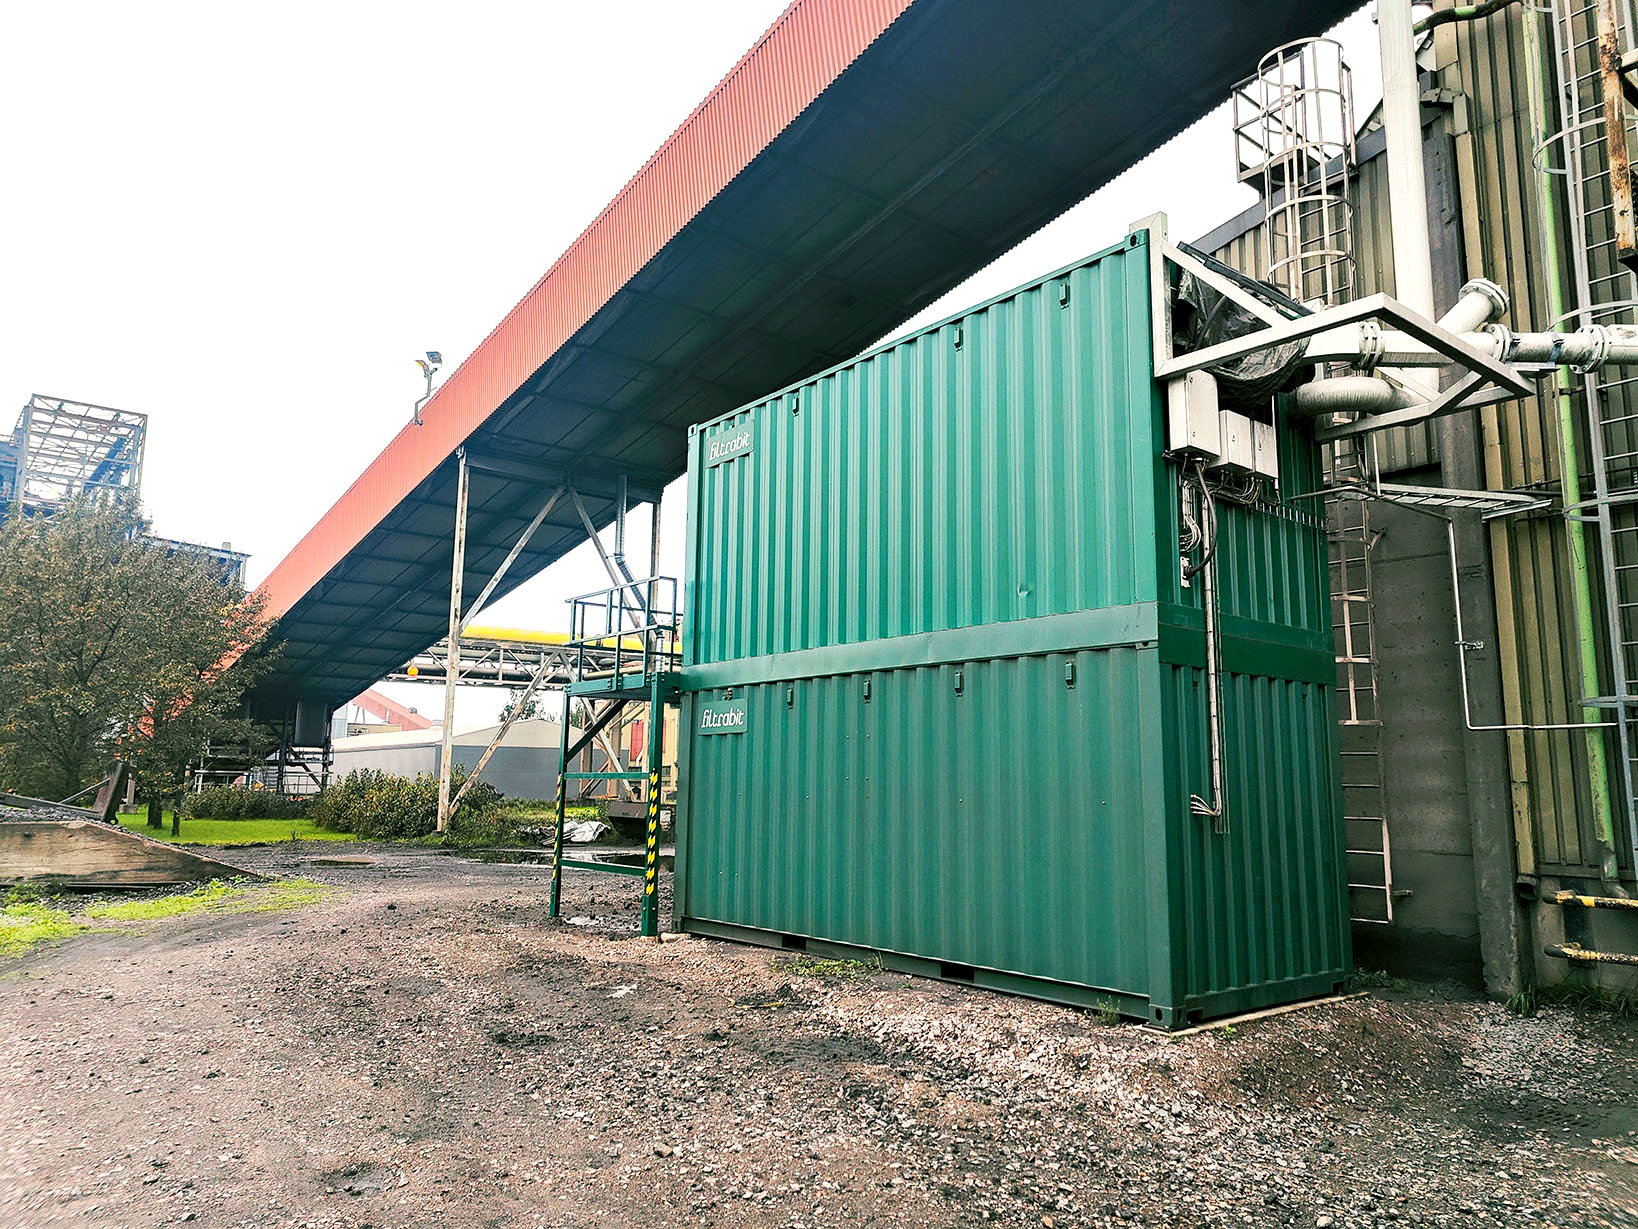
The DC202 and DC402 models are built on a pallet and fit inside a standard shipping container, eliminating the need for significant construction work. Units can be mounted side by side and on top of each other, enabling exact tailoring of capacity.
The compactly sized units are serially produced and portable, allowing for quick installation and a flexible placement close to the source of the dust.
For extremely tight-fitting applications, the units can be installed without the container housing, and split into two separate skid-mounted elements.
High performance
The separation core of the Filtrabit® dust extraction system has been proven to be highly efficient in separating large volumes of different dust types, including abrasive materials like ferrochrome and metallurgical coke.
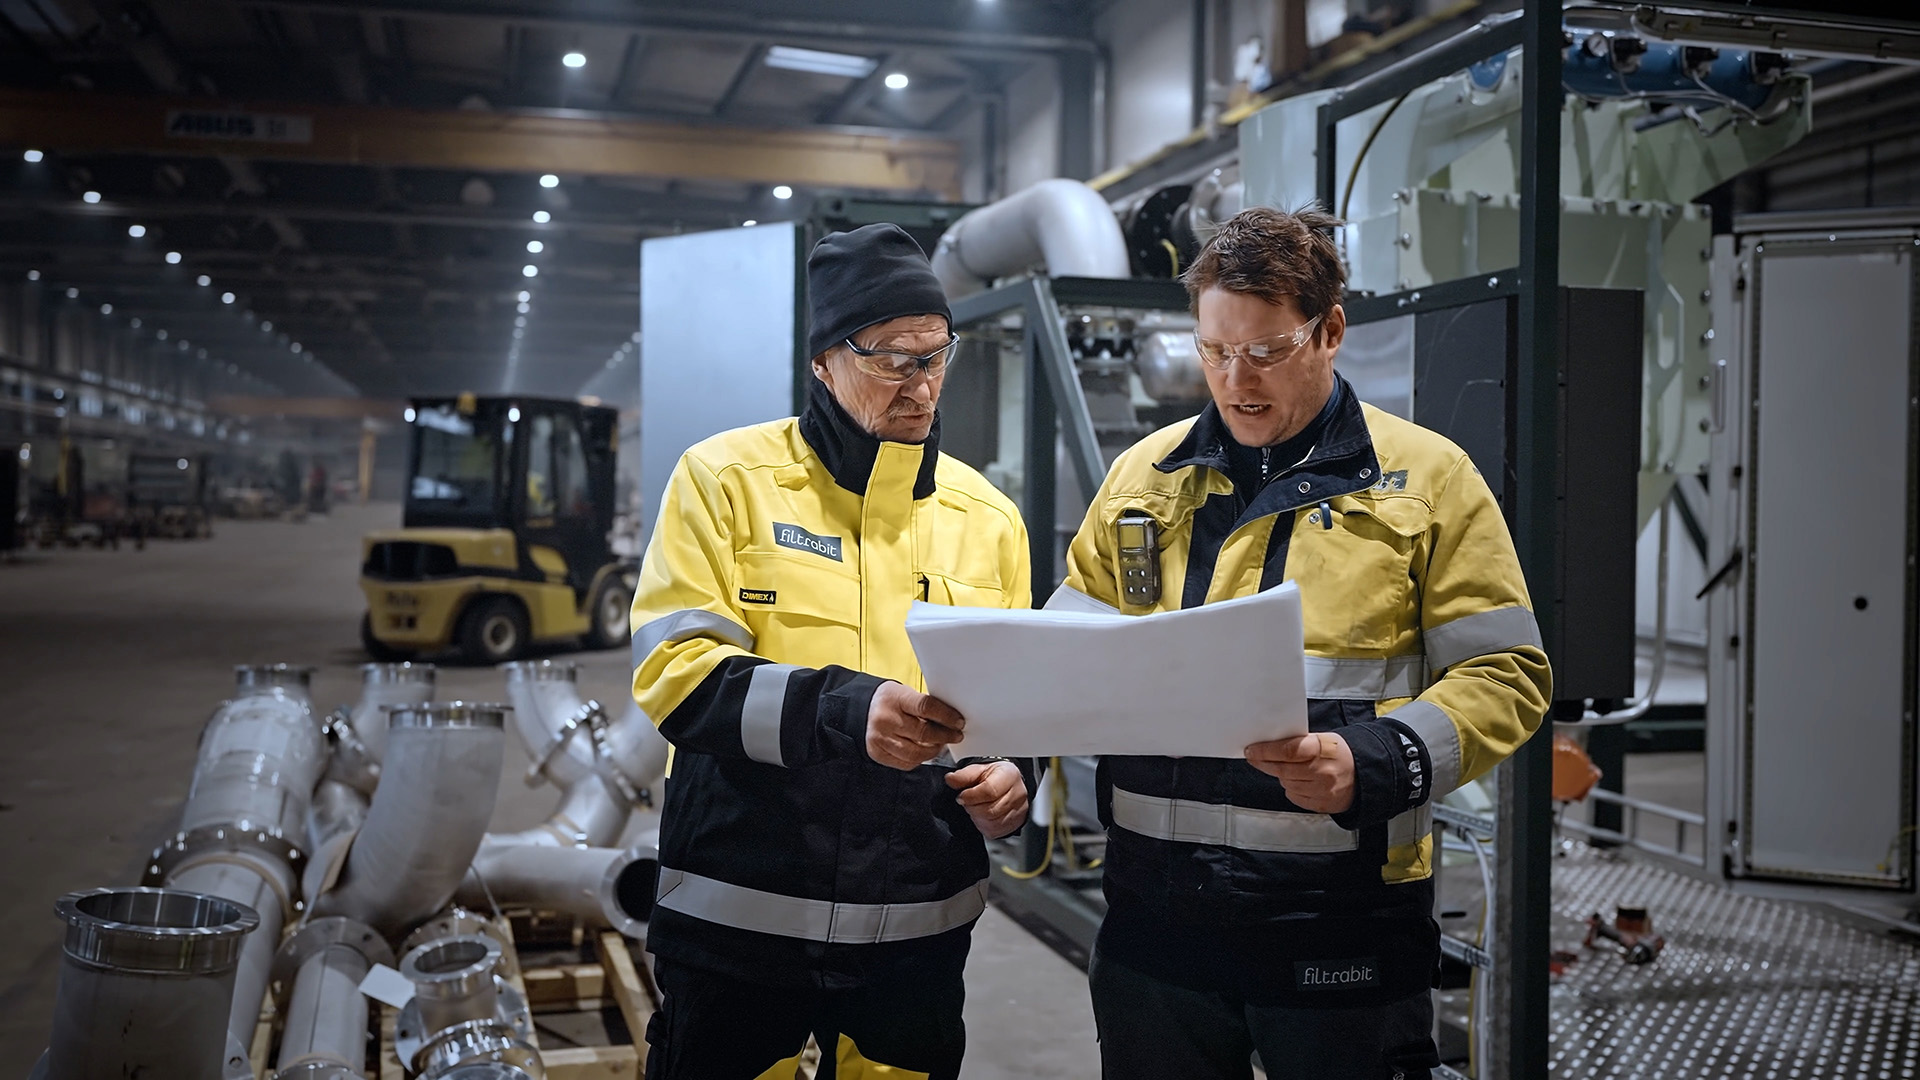
The smaller dual-core model has been measured to extract on average 150 kg of dust per hour in a high-density coke dust application, with peak extraction exceeding 300 kg per hour. Independent testing by Eurofins measured over 99% efficiency for particles larger than 2.5 μm (PM2.5) and over 96% for smaller particles.
Separation efficiency is specific to the application and dependent on properties of the dust and intake gas.
Operational durability and heat resistance
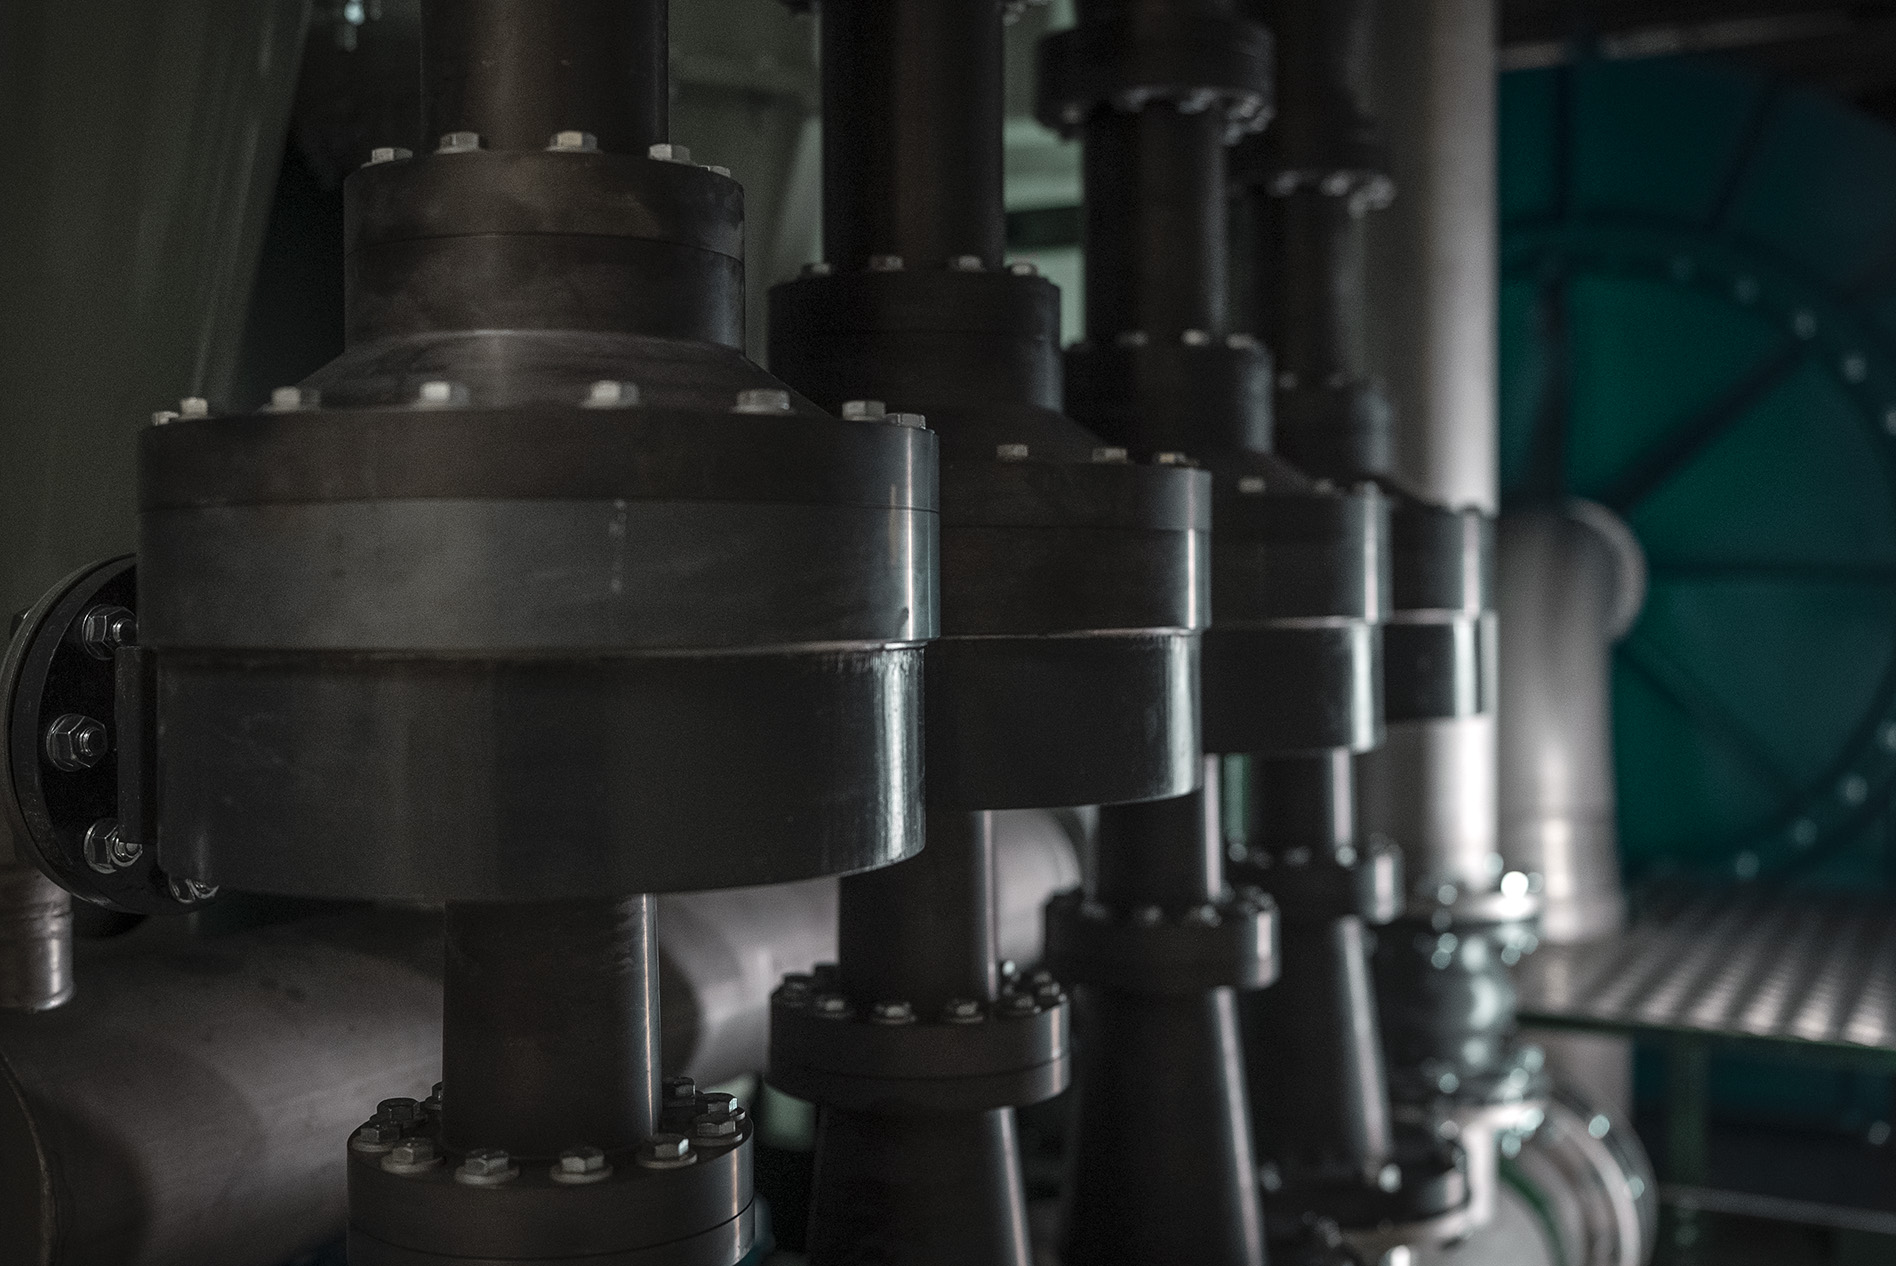
The flow-dynamic dust separators are built from durable steel and are able to handle coarse and abrasive particles without the punctures and clogging common to other, filter-media-based solutions.
A high-temperature modification is also available, capable of handling gas temperatures up to 400 °C.
Dust Removal as a Service
Filtrabit offers dust separation units on an operating lease model and together with partners, helps clients design the necessary hooding and ducting.
The operating lease option eliminates the need for large capital expenditures, helping respond to a constantly moving regulatory environment while unlocking capital for investments into core processes.
Filtrabit is responsible for the maintenance and replacement components for the leased unit, giving the client both financial and operational peace of mind.
Material recovery
Flow-dynamic dust separation technology offers the unique ability to recover raw materials as distinct from one another, before mixing in a centralized system. This side stream helps offset both net CO2 emissions and the leasing cost of the modular unit.
The side stream is collected separately for the coarse and fine fractions, sometimes allowing for more favorable chemical compositions due to a natural sorting effect, if cross-contaminants disproportionately appear as finer fractions, for example.
Even in less valuable materials, the savings from reduced waste management fees can still become substantial, as the uncontaminated material can be immediately returned to the process.
At the Outokumpu Tornio stainless steel plant, a study concluded that the flow-dynamic dust separator unit installed at the alloying station turns a direct profit due to the value of the collected dust and the reduced waste management fees.1
Depending on the client’s needs, the collected material can be continuously conveyed from the flow-dynamic dust separator into a suitable destination, or collected into Flexible Intermediate Bulk Containers on the spot.
1filtrabit.com/study-validates-economic-and-environmental-success-of-filtrabit-at-outokumpu-tornio/

Operating principle
Main parts
Pre-separator cyclone
Separation core
Dust hopper
Centrifugal fan
Dust conveying option
Flow of operation
Dusty air is first pulled into the coarse pre-separation cyclone, which removes the larger particles.
Finer particles continue to the separation core, which extracts them using Filtrabit’s patented method based on flow-dynamics.
Cleaned air proceeds directly to the clean air outlet, while the dusty flow continues on to the dust hopper.
After being separated from residual air, the pure dust is fed into the chosen conveying option, which delivers it out of the system.
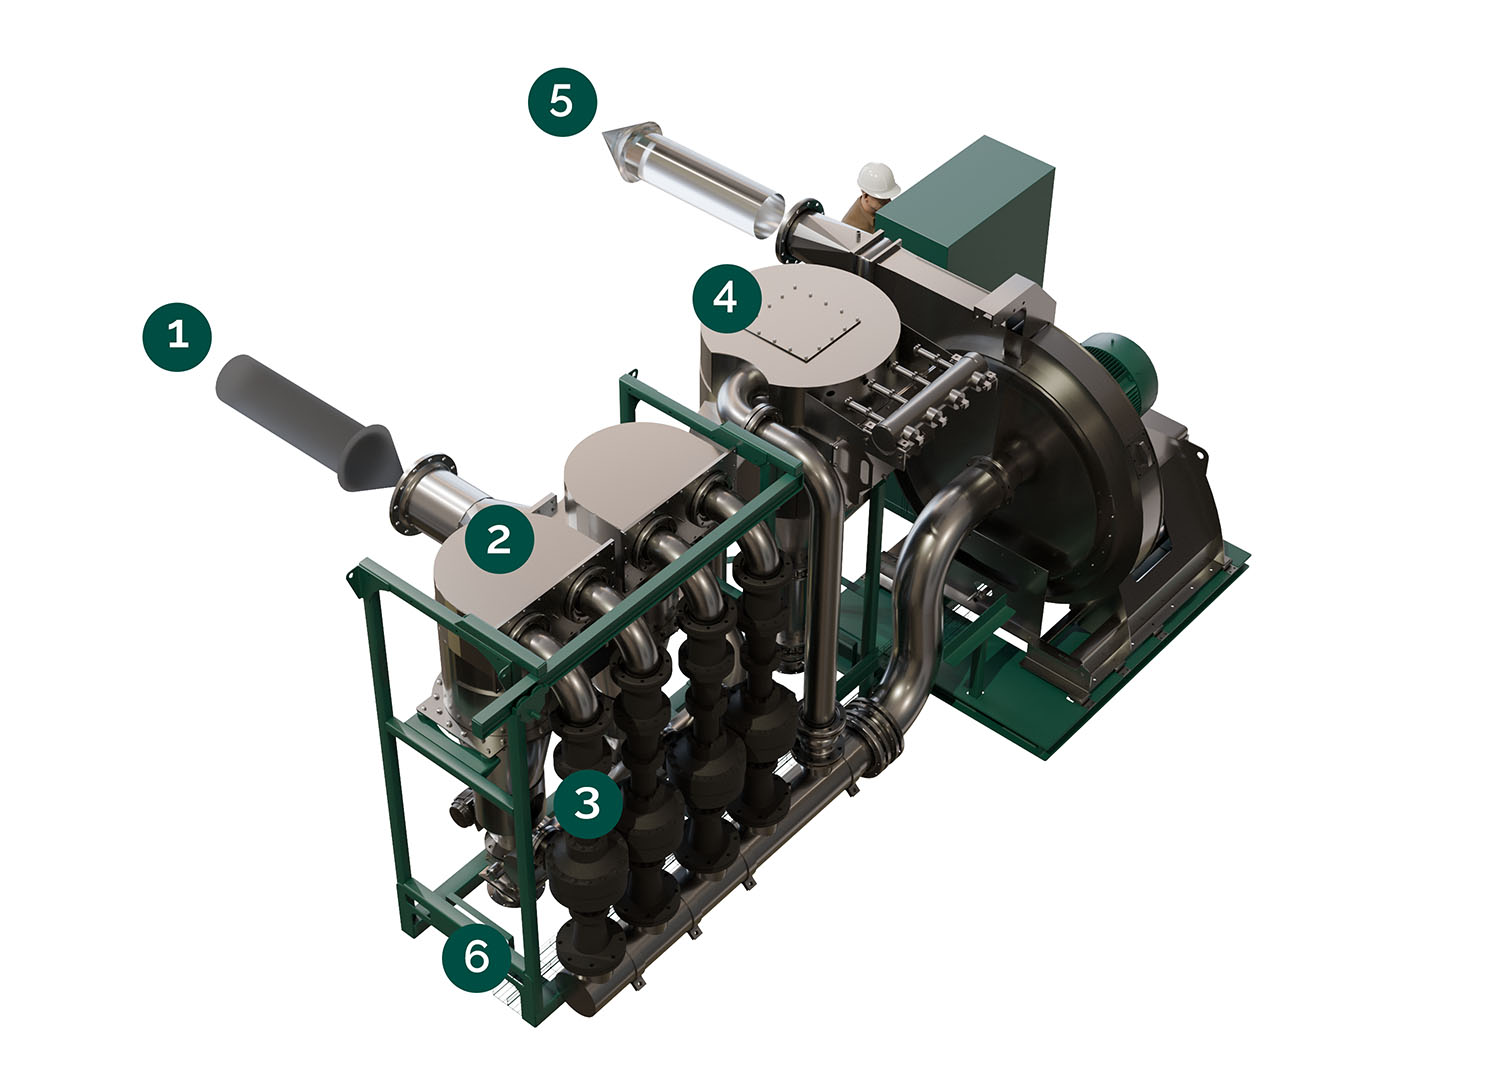
1Dusty gas intake
2Pre-separator removes larger particles
3Separation cores extract fine particles from the stream
4Fine particles are collected into the dust hopper
5Clean gas outlet
6Collected dust is discharged via chosen delivery option
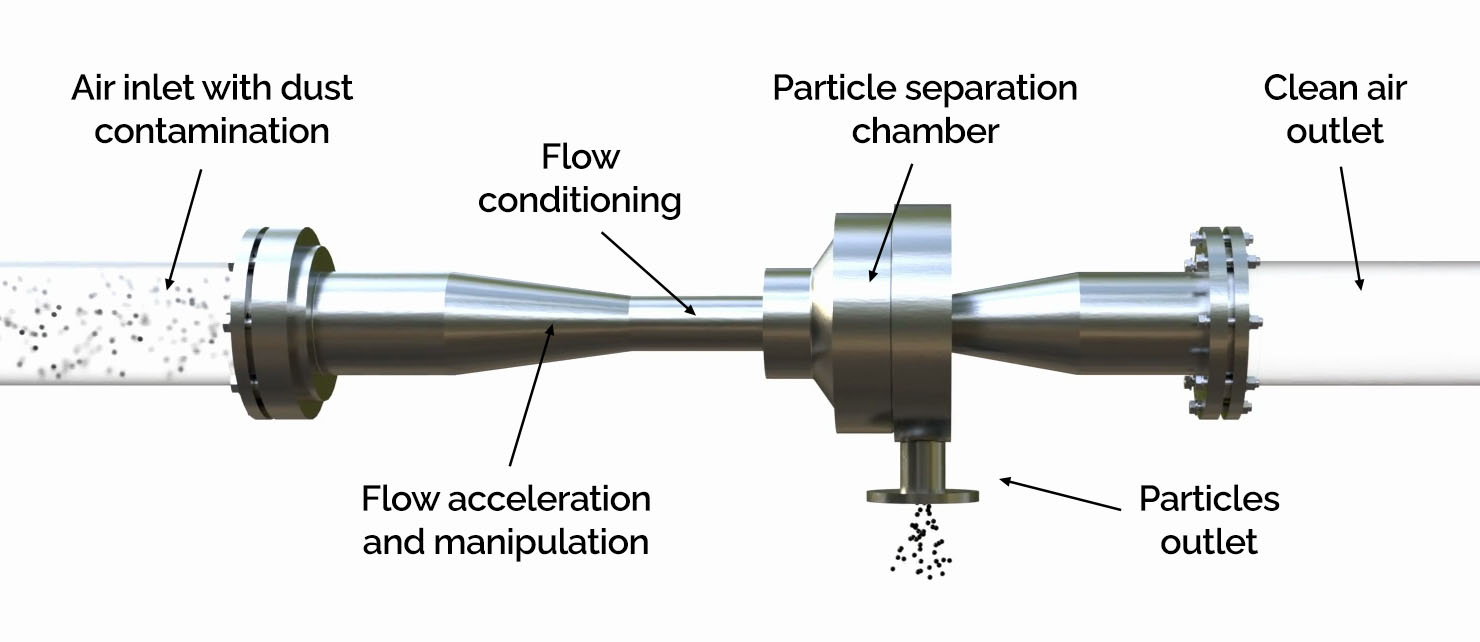
Separation core
In the separation core, gas flow speeds up as it travels through the acceleration zone.
Particles separate by mass and get diverted to a separation chamber, from where the dusty flow continues on to the dust hopper.
Meanwhile, clean air flows directly through the center of the core, on towards the clean air outlet.
Supporting an existing dust control system
A typical application for the system is working concurrently with an existing, centralized dust control system that has been outgrown by increases in the production capacity of the facility.
With smart hooding designs, the high dust density air is prevented from mixing with the ambient air, which minimizes the air volume that needs to be cleaned. This allows for the highest possible dust separation efficiency and reduces the demand on the centralized system.
By preventing the overloading of an existing system, significant savings can be made from extending maintenance intervals and reducing costly production downtime. The performance of the existing system is also markedly improved by the reduction in back pressure as a consequence of taking over one or more demanding intake areas.
At the SSAB Raahe coking plant, the maintenance interval for a 40,000 m3/h bag filter went from 6 months to 2 years after introducing a flow-dynamic dust separator to handle the dustiest intake. A planned multi-million-euro overhaul of the bag filter was cancelled after the successful intervention by flow-dynamic dust separation technology.2
Closed loop solution
In suitable applications, a closed loop solution can be utilized for maximum results. A conveyor transfer point, for example, can be hooded in such a way that the cleaned air is directed back into the exhaust intake from below, creating a push-pull current of air.
This controlled disturbance of air at the desired point inside a hooding enclosure helps loosen the small particles that would be at risk of becoming airborne at a later stage of the process.
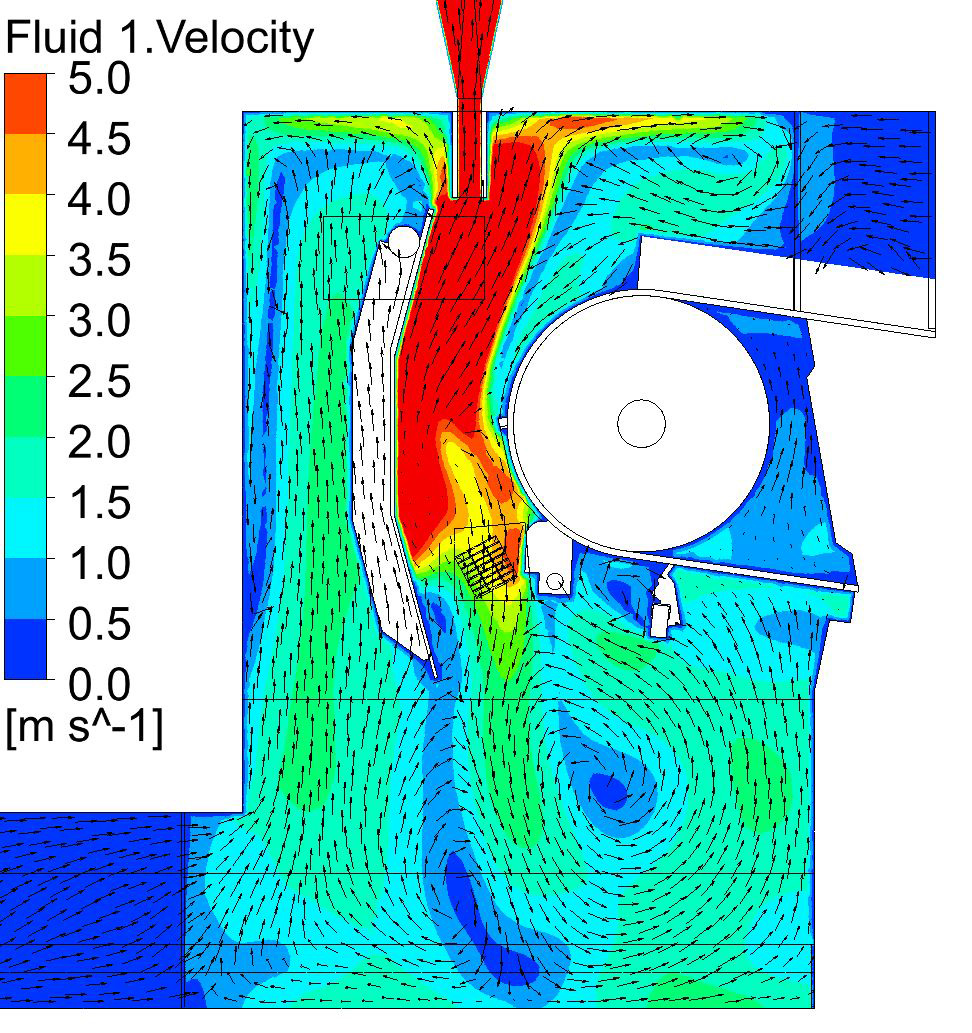
Computational Fluid Dynamics simulation of a conveyor transfer point utilizing a push-pull method of airflow at the exhaust intake, forming a closed loop.
Application areas
Typical dust to be collected is dry and relatively dense, approximately 1 kg/liter or more. As part of the standard process, Filtrabit performs a test on the client’s dust sample and provides clear indication of the separation performance.
Industries
Steel manufacturing
Non-ferrous metals
Mining and minerals
Quarrying
Foundries
Processes
Conveying and feeding materials
Unloading bulk material from ships
Crushing
Sieving
Grinding
Thermal and combustion processes
Technical specifications
| DC202 | DC402 | |
|---|---|---|
| Separation cores | 2 | 4 |
| Gas flow | 2 400 m3 / h | 4 800 m3 / h |
| Gas temperature | -30 °C to 400 °C (configurable within the temperature range) |
|
| Separation performance | 150 kg / h (application specific) |
300 kg / h (application specific) |
| Separation efficiency | >99% for PM2.5 and larger >96% for smaller than PM2.5 (application specific) |
|
| Dimensions (L x W x H) | Skid assembly: 5.16 m x 2.11 m x 2.62 m Container: 6.05 m x 2.44 m x 2.90 m |
|
| Weight | Skid assembly: 4 800 kg / 6 000 kg Container: 5 800-7 300 kg / 7 000-8 500 kg |
|
| Gas connections (inlet/outlet) | DN200 | DN300 |
| Power consumption | 40 kW | 75 kW |
| Particle outlet options |
|
|
| Connectivity to DCS / Factory Automation System (option) | DIO / Industrial Ethernet (Modbus TCP, Profinet protocols) | |
| Remote service platform (option) | Secured VPN & web-based management / remote control, data logging etc. | |
Summary of benefits
Easy retrofit add-on — Seamlessly integrates into specific process points without major construction works
Scalable — Capacity can be adjusted by adding units
Relief for existing emission control systems — Performance boost from adding Filtrabit units into high emitting locations
Proven, robust and reliable — Long maintenance intervals: no clogging or filter punctures
High performance
Dual efficiency — Captures both coarse and fine particles
Handles high dust loads — Consistent performance without added back pressure
Thermal toughness — Outperforms conventional filter restrictions
Material recovery — Onsite separation and direct reuse of captured dry material
CO2 reduction — Offsetting use of virgin resources
Raw material savings — Immediate reusability before mixing with other dusts
Capital-efficient approach — Operating lease model to avoid substantial upfront capital expenditures.
London
- Filtra Group Oy
- 53 Eastlake House Frampton Street
- LONDON NW8 LU
- United Kingdom
- +44 7990 908 822
- +358 46 887 4455
Espoo
- Innopoli 2
- Technopolis
- Tekniikantie 14
- FI-02150 ESPOO
- Finland
Member of:

© 2021–2026 Filtrabit Oy. All rights reserved.
FILTRABIT is a registered trademark of Filtrabit Oy. All rights reserved.